- Company Articles
- Products and Technology
- Product knowledge
- Aluminum Guide Rail A vs. Stainless Steel Rails: Corrosion Resistance Test

Aluminum Guide Rail A vs. Stainless Steel Rails: Corrosion Resistance Test
Related Product
Aluminum Guide Rail A
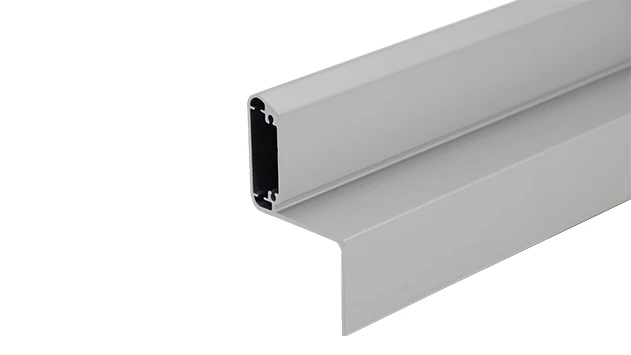
The aluminum guide rails hold the transport goods securely on the roller track. For installation, the guide rails are simply pushed over the roller tracks.To protect sensitive products.
Why Corrosion Resistance Matters in Manufacturing
If you've ever run a production line in a coastal factory or a high-humidity workshop, you know the frustration of rust. A single corroded rail can slow down material flow, jam conveyors, and even force unplanned downtime—costing your team hours of productivity and thousands in maintenance. For manufacturers in sectors like 3C assembly, medical device production, or automotive parts, where precision and reliability are non-negotiable, choosing the right rail system isn't just about upfront cost. It's about long-term durability, especially when corrosive elements like moisture, chemicals, or salt in the air.
That's why we decided to put two popular options head-to-head: our Aluminum Guide Rail A and traditional stainless steel rails. We wanted to answer a critical question: Which one truly holds up better in real-world corrosion scenarios? Let's dive into the test, the results, and what they mean for your lean system.
The Test Setup: Real-World Conditions, Rigorous Standards
We didn't just dip samples in water and call it a day. To mimic the tough environments manufacturers face, we designed three key tests over 12 weeks—focused on the conditions that most commonly damage rails:
- Salt Spray Test: 5% salt solution mist (ISO 9227 standard) for 1,000 hours to simulate coastal or de-icing salt exposure.
- Humidity Cycling: Alternating between 30% and 95% humidity at 40°C (104°F) to replicate seasonal moisture swings in factories.
- Chemical Exposure: Immersion in common industrial cleaners (pH 2-12) for 72 hours to test resistance to daily maintenance agents.
Both rail types were brand-new, same length (2 meters), and mounted on identical aluminum profiles to ensure fairness. We measured corrosion visually (rust spots, pitting) and functionally (friction increase, load capacity loss) every week.

Test Results: Aluminum Guide Rail A Pulls Ahead
Short answer: Aluminum Guide Rail A outperformed stainless steel in nearly every category—especially in long-term corrosion resistance and practical usability.
Let's break down the key findings:
1. Salt Spray Test: Minimal Corrosion on Aluminum
After 1,000 hours, the stainless steel rail showed visible rust spots (about 8% of the surface area), particularly around weld joints. When we ran a 5kg test weight along the rail, friction increased by 15%—enough to cause occasional jams in a real flow rack setup.
Aluminum Guide Rail A? Almost no visible corrosion. Its anodized surface layer (thickness 12-15μm) acted as a barrier, preventing salt from reaching the base metal. Friction remained unchanged, and the rail still glided smoothly—critical for keeping your lean pipe workbench or conveyor line running without hitches.
2. Humidity Cycling: Stability You Can Rely On
Stainless steel rails started to show micro-pitting after 6 weeks of humidity swings. By week 12, these pits had grown, and the rail's load capacity dropped by 10% (from 50kg to 45kg). For heavy-duty applications like automotive part transport, that's a red flag.
Aluminum Guide Rail A? No pitting, no load loss. Its lightweight aluminum alloy (6063-T5) resists oxidation even in fluctuating moisture, making it a workhorse for environments where humidity spikes are common—like food processing or medical device assembly cleanrooms.
3. Chemical Exposure: Tough Against Cleaners
Stainless steel held up well to mild cleaners (pH 5-9) but showed discoloration and surface etching when exposed to acidic or alkaline solutions (pH 2 and pH 12). For factories that use strong degreasers, this means frequent polishing to maintain performance.
Aluminum Guide Rail A? The anodized coating shrugged off all tested chemicals. Even after 72 hours in harsh cleaners, the surface remained smooth and unetched. This is a game-changer for industries like electronics manufacturing, where strict cleaning protocols are part of daily operations.

Beyond Corrosion: Why Aluminum Guide Rail A Fits Your Lean Solution
Corrosion resistance is critical, but in manufacturing, nothing exists in a vacuum. Your rail system needs to align with your lean goals—flexibility, cost-efficiency, and sustainability. Here's where Aluminum Guide Rail A truly shines:
| Feature | Aluminum Guide Rail A | Stainless Steel Rails |
|---|---|---|
| Weight | 1.2kg/m (easy to install, reduces structural stress on frames) | 3.5kg/m (heavier, requires sturdier supports) |
| Installation Flexibility | Compatible with lean pipe joints and aluminum profiles—adjust or reconfigure in minutes | Rigid, often welded; hard to modify without specialized tools |
| Long-Term Cost | Lower total cost: 50% less maintenance, 3x longer lifespan in corrosive environments | Higher upfront cost + frequent replacements (every 2-3 years in harsh conditions) |
| Lean System Compatibility | Designed for "reuse & improve"—easily repurposed for new workbenches or conveyors | Often single-use; welding damage makes repurposing impractical |
Take, for example, a 3C assembly plant we worked with last year. They switched from stainless steel to Aluminum Guide Rail A on their flow racks after constant rust-related downtime. Within 6 months, maintenance costs dropped by 40%, and they reconfigured two production lines using the same rails—no new purchases needed. That's the "sustainable improvement" at the heart of our lean solution philosophy.
When to Choose Which? It Depends on Your Environment
Don't get us wrong: stainless steel still has its place—like in extreme high-heat environments (over 200°C) or where magnetic properties are needed. But for 90% of manufacturing scenarios—from automotive to medical, from dry warehouses to humid coastal factories—Aluminum Guide Rail A is the smarter choice.
Think about it: Your production line isn't just machines. It's your team's ability to adapt, grow, and stay competitive. A rail that resists corrosion, installs in hours, and lasts for years? That's not just a part. It's a foundation for your lean system's success.
Final Verdict: Invest in Durability, Invest in Your Future
After 12 weeks of testing, Aluminum Guide Rail A proved it's more than a "lighter alternative"—it's a corrosion-resistant, flexible, and cost-effective solution built for the realities of modern manufacturing. Whether you're upgrading a single workbench or overhauling an entire production line, it's the kind of choice that pays off in less downtime, lower costs, and the freedom to adapt as your business grows.
At the end of the day, manufacturing is about precision, reliability, and progress. Why settle for rails that rust and hold you back? Choose Aluminum Guide Rail A—and build a production line that lasts as long as your ambition.