- Company Articles
- Products and Technology
- Product knowledge
- Cost-Benefit Analysis: Aluminum Guide Rail A vs. Carbon Steel Rails Over Time

Cost-Benefit Analysis: Aluminum Guide Rail A vs. Carbon Steel Rails Over Time
Related Product
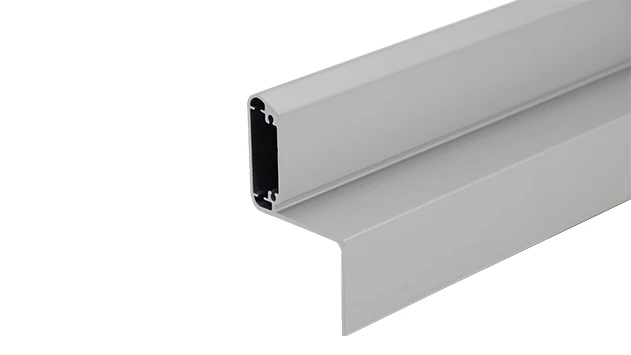
Aluminum Guide Rail A
The aluminum guide rails hold the transport goods securely on the roller track. For installation, the guide rails are simply pushed over the roller tracks.To protect sensitive products.
In the fast-paced world of manufacturing, every component in your production line plays a silent but critical role in keeping operations running smoothly. From the smallest caster wheel to the longest conveyor belt, the choices you make today can either build a foundation for long-term efficiency or create hidden costs that chip away at your bottom line over time. When it comes to material handling—especially in high-demand sectors like 3C assembly, medical device production, or warehousing—one component stands out for its quiet impact: guide rails. These unassuming structures are the backbone of seamless workflow, guiding everything from circuit boards on an ESD workstation to heavy components on a flow rack. But here's the question manufacturers often grapple with: Aluminum Guide Rail A or traditional carbon steel rails? Let's dive into a real-world cost-benefit analysis that goes beyond the price tag and looks at how these two options perform over years of hard use.
First Things First: What Are We Comparing?
Before we crunch numbers, let's get clear on what each rail brings to the table. Aluminum Guide Rail A, a staple in modern lean system setups, is engineered from high-grade aluminum extrusion profile—lightweight, corrosion-resistant, and designed for modular flexibility. It's the kind of rail you'll find in Workbench E setups or integrated into Material Rack B, where adaptability and durability matter most. On the other side, carbon steel rails are the old reliable—sturdy, familiar, and often cheaper upfront. They've been around for decades, used in everything from basic roller tracks to heavy-duty conveyors. But as any plant manager who's dealt with rusted joints or frequent replacements will tell you, "cheap upfront" doesn't always mean "cost-effective long-term."
The Cost Breakdown: Beyond the Initial Price Tag
Let's start with the numbers everyone notices first: initial cost. It's true—carbon steel rails often come with a lower sticker price. For example, a 3-meter section of basic carbon steel rail might cost 30-40% less than Aluminum Guide Rail A. If you're equipping a small workshop or working with a tight immediate budget, that difference can feel significant. But here's where the story gets interesting: manufacturing isn't a one-time purchase. It's a long-term investment, and costs stack up in ways that aren't always obvious on day one. Let's break it down into four key areas:
1. Maintenance: The Hidden Drain on Carbon Steel
Walk into a facility that's been using carbon steel rails for 5+ years, and you'll likely spot the signs: rust patches eating through paint, stiff joints that require frequent lubrication, and bent sections from heavy use. Carbon steel is tough, but it's not immune to the elements—especially in environments with moisture, like food processing or medical device plants, or with chemicals, like in automotive painting shops. To keep carbon steel rails functional, you're looking at regular upkeep: annual painting or coating (around $2-3 per linear foot), monthly lubrication for moving parts, and occasional repairs to fix warped sections. Over 10 years, that adds up to roughly $15-20 per linear foot in maintenance costs alone.
Aluminum Guide Rail A, on the other hand, is a low-maintenance workhorse. Thanks to its natural corrosion resistance, it doesn't need painting or anti-rust treatments. Its smooth aluminum extrusion profile minimizes friction, so lubrication is rarely required. Even in humid warehouses or cleanrooms, it holds up without degradation. Most manufacturers report spending less than $1 per linear foot over 10 years on maintenance—mostly just occasional cleaning. For a 100-foot production line, that's a 10-year maintenance saving of $1,400-1,900 with aluminum.
2. Replacement Cycles: How Long Until You're Buying Again?
Carbon steel rails typically have a lifespan of 5-7 years in heavy-use environments. After that, rust weakens their structural integrity, and repeated bending or impact makes them unreliable. Replacing a full set of rails means downtime—tearing out old sections, installing new ones, and recalibrating the flow of materials. For a mid-sized facility with 500 feet of rail, that's a replacement cost of $15,000-20,000 every 5 years, plus 2-3 days of lost production (which, for a plant with daily output worth $10,000, adds another $20,000-30,000 in downtime costs).
Aluminum Guide Rail A, built from high-strength aluminum profile, lasts 15-20 years under the same heavy conditions. Its flexibility means it bends without breaking, and its resistance to corrosion ensures it stays strong over time. That means instead of replacing rails every 5 years, you're looking at a single replacement cycle every 15-20 years. Over 20 years, carbon steel would require 3-4 replacements, while aluminum needs just 1. The math here is stark: carbon steel ends up costing 3-4x more in replacement and downtime over two decades.
3. Energy Efficiency: Lighter Rails, Lower Bills
Here's a factor many overlook: weight. Aluminum is 30% lighter than carbon steel. When you're moving materials along a flow rack or conveyor, that lighter weight translates to less energy needed to power motors or push carts. For example, a conveyor system using aluminum rails requires smaller motors and uses 15-20% less electricity than one with carbon steel rails. Over a year, that could mean savings of $500-1,000 per conveyor. Multiply that by 10 conveyors in a large facility, and you're looking at $5,000-10,000 in annual energy savings—savings that add up exponentially over time.
4. Installation: Time is Money (and Aluminum Saves Both)
Installing carbon steel rails is labor-intensive. Their weight means you need more workers or specialized lifting equipment, and their rigidity makes alignment tricky. A team of 4 might take 8 hours to install 100 feet of carbon steel rail. Aluminum Guide Rail A, being lighter and modular (thanks to components like internal rotary aluminum joints), can be installed by 2 workers in 4 hours for the same 100 feet. That's 50% less labor time, which translates to $800-1,200 saved per 100 feet in installation costs alone. Plus, faster installation means less downtime during setup—getting your production line up and running sooner.

The Benefit Side: Why Aluminum Guide Rail A Delivers More Than Just Savings
Cost is only half the equation. The real value of a component lies in how it improves your operations—making your team more efficient, your processes more flexible, and your business more adaptable to change. Here's where Aluminum Guide Rail A truly shines, especially when paired with a lean system approach.
1. Flexibility: Adapt or Get Left Behind
Modern manufacturing moves fast. Product lines change, order volumes fluctuate, and new technologies require reconfigured workspaces. Carbon steel rails, being rigid and often welded in place, are hard to modify. Want to add a new branch to your flow rack or reposition a conveyor? You'll likely need to cut and reweld steel, which is time-consuming and costly. Aluminum Guide Rail A, though, is designed for the lean (lean philosophy) of "sustainable improvement." Its modular design—using components like aluminum guide rail connectors and placon mounts—lets you disassemble, reconfigure, and reuse rails in new setups. For example, a 3C assembly plant that switches from producing smartphones to tablets can rework their aluminum rail system in a day, whereas a carbon steel setup might take a week or more. That agility lets you respond to market changes faster, winning more orders and staying ahead of competitors.
2. Durability in Harsh Environments
In industries like medical device manufacturing or food processing, cleanliness and corrosion resistance are non-negotiable. Carbon steel rails, even with coatings, can harbor bacteria in rust crevices or react with cleaning chemicals. Aluminum Guide Rail A, being naturally resistant to corrosion and easy to sanitize, meets strict industry standards for hygiene. A medical equipment manufacturer in California reported a 40% reduction in contamination-related downtime after switching to aluminum rails, simply because the rails stayed cleaner and required fewer deep-cleaning sessions.
3. Worker Satisfaction: Smooth Workflows Mean Happier Teams
It's easy to overlook, but the tools your team uses every day affect morale and productivity. Stiff, rusted carbon steel rails can cause jams, slow down material flow, and lead to frustrating delays. Aluminum Guide Rail A, with its smooth roller tracks and lightweight design, creates a workflow that feels effortless. Workers spend less time wrestling with stuck parts and more time focused on value-adding tasks. A survey of plant floor employees at a automotive parts manufacturer found that after switching to aluminum rails, 78% reported feeling less stressed, and productivity increased by 12%—a win for both your team and your bottom line.

The Long-Term Comparison: A 15-Year Case Study
Let's put all this together with a real-world example. Imagine a mid-sized electronics manufacturer (3C assembly) with 1,000 feet of guide rails across 10 flow racks and 5 conveyors. Let's compare the total cost of ownership for Aluminum Guide Rail A vs. carbon steel over 15 years:
| Cost Category | Carbon Steel Rails | Aluminum Guide Rail A | Difference (Aluminum Savings) |
|---|---|---|---|
| Initial Cost (1,000 ft) | $25,000 | $40,000 | -$15,000 (Higher upfront) |
| Maintenance (15 years) | $15,000 (1,000 ft x $1/ft/year x 15) | $1,500 (1,000 ft x $0.10/ft/year x 15) | +$13,500 |
| Replacement (15 years) | $75,000 (3 replacements x $25,000) | $40,000 (1 replacement) | +$35,000 |
| Downtime (15 years) | $90,000 (3 replacements x 3 days x $10,000/day) | $30,000 (1 replacement x 3 days x $10,000/day) | +$60,000 |
| Energy Savings (15 years) | $0 | $75,000 (5 conveyors x $1,000/year x 15) | +$75,000 |
| Total 15-Year Cost | $205,000 | $146,500 | +$58,500 |
After 15 years, the aluminum system—despite its higher initial cost—saves the manufacturer $58,500. And that's not even counting intangible benefits like faster reconfiguration, higher worker productivity, or better compliance with industry standards. For a business, that's not just savings—it's capital that can be reinvested in new technology, employee training, or expanding operations.
When Does Carbon Steel Still Make Sense?
We'd be remiss not to acknowledge cases where carbon steel might still be the right choice. If you're running a temporary facility with a lifespan of less than 5 years, or if you're working with extremely heavy loads (over 500kg per linear foot) where steel's rigidity is non-negotiable, carbon steel could be a practical short-term solution. But for 90% of manufacturers—especially those focused on lean system principles, sustainability, and long-term growth—Aluminum Guide Rail A is the clear winner.
Conclusion: Invest in What Grows With You
At the end of the day, choosing between Aluminum Guide Rail A and carbon steel rails isn't just about rails—it's about choosing a partner for your business's future. Carbon steel offers quick savings today, but it's a short-term fix that costs more down the line. Aluminum Guide Rail A, though requiring a larger initial investment, pays dividends for decades through lower maintenance, fewer replacements, energy savings, and unmatched flexibility. It aligns with the lean of "doing more with less" and "sustainable improvement," helping you build a production line that adapts, endures, and grows with your business.
So, the next time you're evaluating material handling components, remember: the best choice isn't always the cheapest one today. It's the one that keeps working for you tomorrow, next year, and long into the future. For most manufacturers, that choice is clear: Aluminum Guide Rail A isn't just a rail—it's an investment in efficiency, durability, and success.