- Company Articles
- Products and Technology
- Product knowledge
- Understanding Friction and Speed Control in 85 Steel Roller Track Systems

Understanding Friction and Speed Control in 85 Steel Roller Track Systems
Related Product
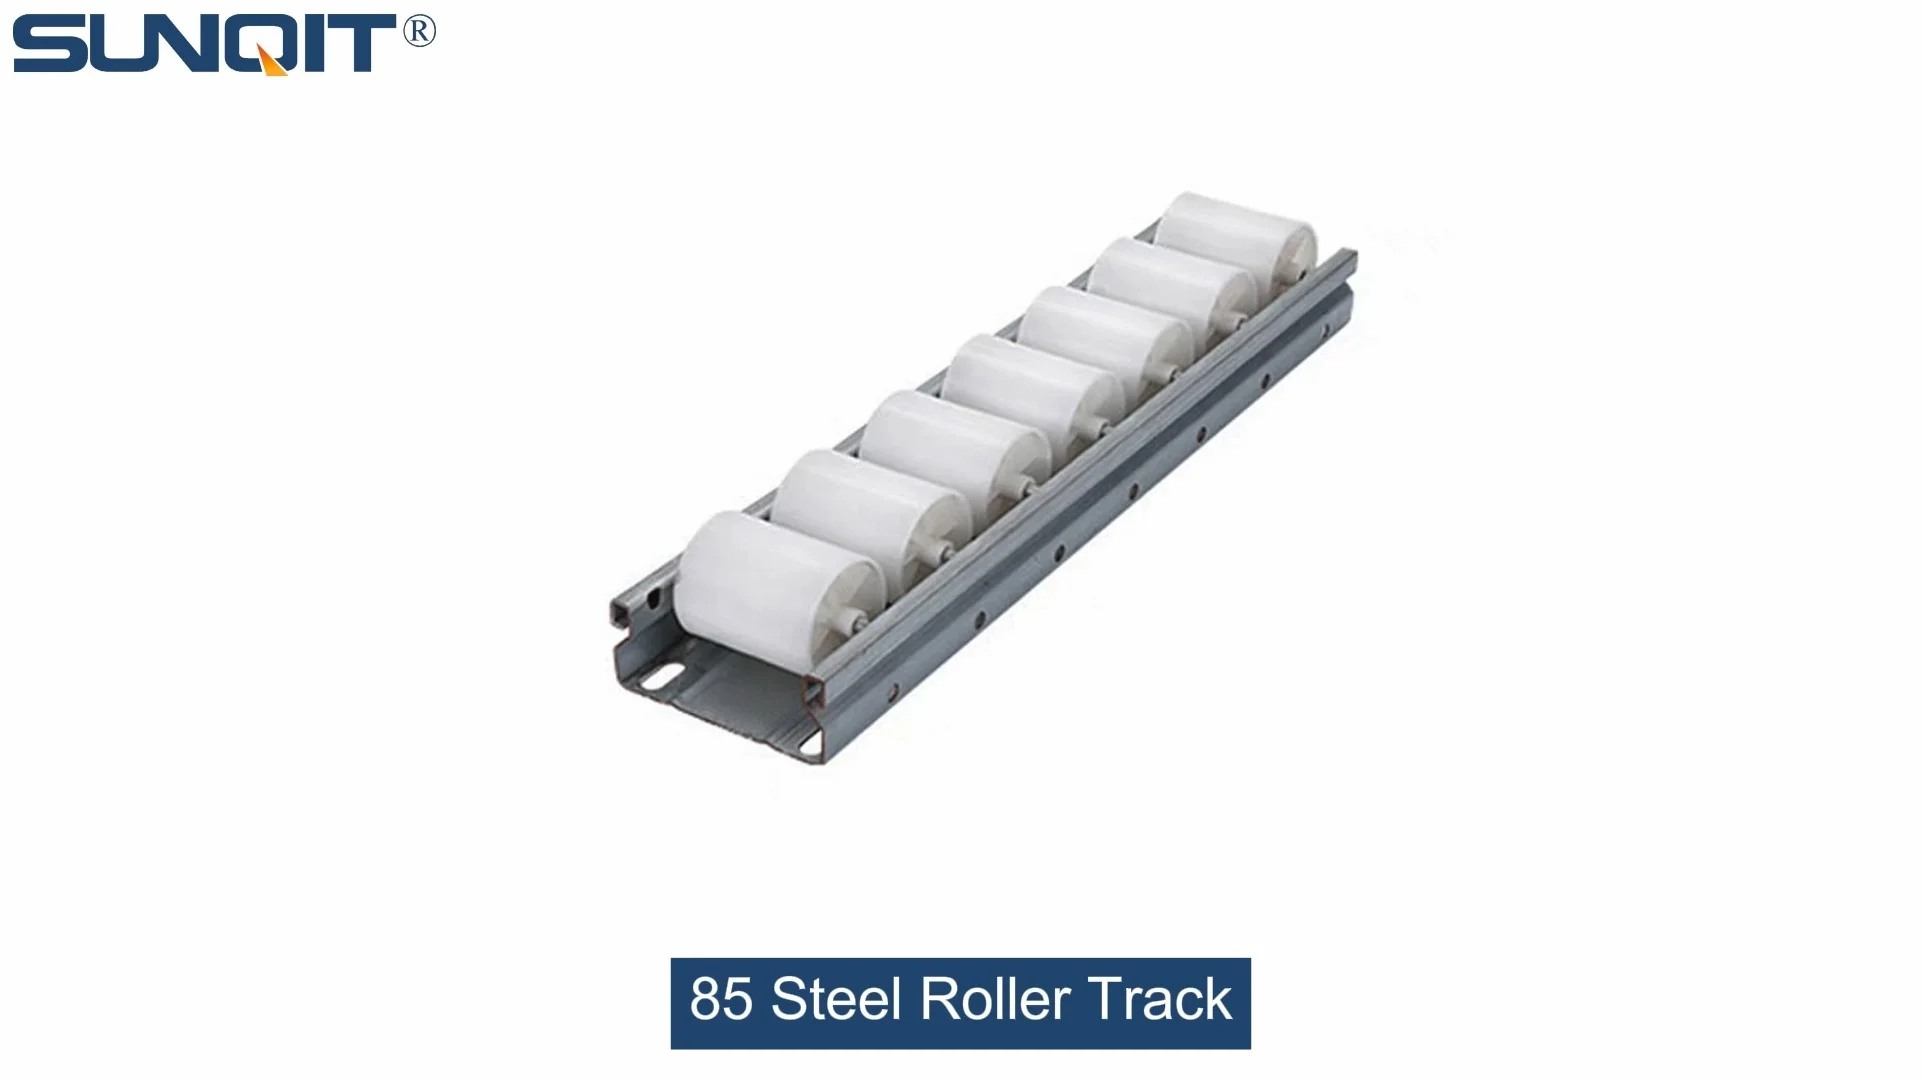
85 Steel Roller Track
85 heavy duty modular system roller track.Its use is focused on the transport of heavy products. Its implantation is carried out by creating a slope for the product to move under the force of gravity.
In the heart of every manufacturing facility, there's an unsung hero working behind the scenes: the roller track. It's the silent conveyor of progress, moving parts from assembly lines to packaging stations, ensuring that production keeps pace with demand. But not all roller tracks are created equal—especially when we're talking about the 85 steel roller track, a workhorse in heavy-duty applications like automotive manufacturing and large-scale assembly. Today, we're diving deep into two critical factors that make or break these systems: friction and speed control. Because when these two elements are in harmony, your production line doesn't just run—it flows .
Why Friction Matters More Than You Think
Let's start with the basics: friction is the resistance that slows down motion when two surfaces rub against each other. In an 85 steel roller track system, this means the difference between a smooth glide and a frustrating jam. Imagine a scenario where a batch of engine components needs to move from the welding station to the painting booth. If friction is too high, those parts might get stuck mid-transit, causing delays that ripple through the entire shift. Too low, and they might slide too fast, crashing into the next station or damaging delicate components. So, what exactly influences friction in these systems?
1. The Materials in Play
The first culprit (or ally) is the material of the rollers and the track itself. 85 steel roller tracks, as the name suggests, use steel rollers, but the wheels can vary—think steel, plastic, or even aluminum. For example, a 40 steel roller track with yellow wheels might have a different friction coefficient than one with black ESD wheels. Plastic roller track guide rails, like the yellow or grey variants often seen in flow racks, are gentler on sensitive parts but tend to create more friction than steel. This is why choosing the right wheel material for your load and part type is like picking the right shoes for a hike—you wouldn't wear sandals on a rocky trail, and you wouldn't use plastic wheels for heavy cast-iron parts.
2. Load and Weight Distribution
Friction isn't static; it changes with how much weight you're putting on the track. A fully loaded material rack B (with 3 rows and 3 floors) will exert more pressure on the rollers than a single lightweight component. This increased pressure can cause the wheels to deform slightly, raising friction. That's why manufacturers like to talk about "load capacity per roller"—it's not just about strength, but about maintaining consistent friction across the system.
3. Lubrication and Maintenance
Even the best steel roller track needs a little TLC. Without proper lubrication, the metal-on-metal contact between rollers and axles can create excessive friction, leading to wear and tear. Think of it like a door hinge that squeaks—ignore it, and eventually, it sticks. Regularly applying the right lubricant (avoiding heavy oils that attract dust) keeps things moving smoothly. Similarly, debris like metal shavings or packaging materials can get caught between rollers, acting like tiny brakes. A quick sweep at the end of each shift can save hours of troubleshooting later.
Mastering Speed Control: It's All About Balance
Once you've got a handle on friction, the next piece of the puzzle is speed control. In manufacturing, speed isn't just about going fast—it's about going consistently . A roller track that sends parts zipping along at 2 meters per second might sound efficient, but if they arrive at the next station faster than the operator can process them, you've just created a bottleneck. So how do engineers dial in the perfect speed?
1. Slope and Incline Design
Many roller tracks rely on gravity to move parts, which means the slope of the track is a key factor. A steeper incline increases speed, but too steep, and you risk damaging parts or losing control. For example, an 85 staggered roller track (designed to reduce friction by staggering rollers) might only need a 2° incline to move heavy parts, while a standard 40 steel roller track might need 3-4°. It's a delicate balance—engineers often test different slopes with mock loads to find the sweet spot.
2. Brakes and Damping Systems
For more precise control, especially in automated lines, braking systems come into play. These can be simple mechanical brakes (like rubber pads that press against the rollers) or advanced sensors that adjust speed in real time. In ESD workstations, where static-sensitive electronics are handled, even small speed fluctuations can cause static buildup—so damping systems that slow parts gradually are a must. It's like hitting the brakes in a car: you don't slam them unless you want to skid.
3. Roller Spacing and Alignment
Believe it or not, how far apart the rollers are placed affects speed too. If rollers are too close together, parts might "bounce" between them, creating uneven motion. Too far apart, and longer parts could sag, increasing friction. The 85 steel roller track, with its larger roller diameter, often requires wider spacing than a mini aluminum roller track. Alignment is just as crucial—if the track is even slightly crooked, parts will veer off course, slowing down as they rub against the side rails.

Real-World Success: When Friction and Speed Work in Harmony
Let's ground this in a real example. A leading automotive manufacturer was struggling with bottlenecks in their transmission assembly line. Parts were arriving at the final inspection station too slowly, causing operators to fall behind. Their old roller track used plastic wheels, which had worn down over time, increasing friction. We recommended switching to an 85 steel roller track with black ESD wheels (to handle static from oily components) and adjusted the slope from 3° to 2.5°. We also added a simple damping brake at the end of the track to slow parts gently before they reached the inspection table. The result? A 20% increase in throughput, and operators reported less fatigue from waiting on parts.
Another case: a 3C assembly plant using flow racks to feed components to the production line. Their plastic roller track guide rails were getting clogged with dust from circuit boards, leading to inconsistent speeds. By switching to a 40 steel roller track with yellow wheels (more durable and easier to clean) and implementing a weekly lubrication schedule, they reduced jams by 75%. It's these small, targeted adjustments that turn a problematic system into a lean solution.

Choosing Your 85 Steel Roller Track: A Quick Guide
Now that you know the "why," let's talk about the "how"—how to pick the right 85 steel roller track for your needs. Here's a breakdown of key considerations:
| Factor to Consider | Best For… | Example Product |
|---|---|---|
| Heavy loads (50kg+ per roller) | Automotive, industrial machinery | 85 steel roller track (staggered or standard) |
| ESD-sensitive parts | Electronics, medical devices | 40 steel roller track with black ESD wheels |
| Lightweight, frequent movement | 3C assembly, packaging | 38 aluminum roller track with yellow wheel flange |
| Outdoor or humid environments | Warehousing, logistics yards | Stainless steel swivel roller balls (1 inch) |
Remember, it's not just about the track itself—think about the entire system. Will it integrate with your existing conveyor or flow rack? Does the supplier offer custom solutions for odd angles or tight spaces? A good lean solution isn't just a product; it's a system that grows with your needs.

Keeping Your System Running Smoothly: Maintenance Tips
Even the best roller track won't last forever without care. Here are a few pro tips to extend its life and keep friction/speed in check:
- Clean regularly: Use a soft brush or compressed air to remove debris from between rollers. Avoid water unless the track is stainless steel—moisture can cause rust.
- Lubricate strategically: Apply a light machine oil to roller axles every 2-4 weeks (more often in dusty environments). Wipe off excess to prevent attracting dirt.
- Check for wear: Inspect wheels for cracks or flat spots, and replace any that look damaged. A worn wheel can throw off the entire system's balance.
- Realign annually: Over time, tracks can shift due to vibration. Use a level to ensure it's still straight, and adjust mounting brackets if needed.
Looking Ahead: The Future of Roller Track Systems
As manufacturing gets smarter, so too will roller track systems. Imagine sensors embedded in the rollers that monitor friction in real time, sending alerts to your maintenance team before a jam occurs. Or AI-driven systems that adjust the slope or braking automatically based on the weight of incoming parts. We're already seeing early versions of this in high-end lean solutions, and it's only a matter of time before these features become standard.
But even with all this technology, the basics remain the same: friction and speed control are the foundation of a smooth-running system. Whether you're using a simple flow rack or a fully automated conveyor line, getting these right will always be the key to unlocking efficiency.
Wrapping Up: Friction and Speed—Your Production Line's Best Friends
At the end of the day, 85 steel roller track systems are more than just metal and wheels—they're the circulatory system of your manufacturing facility. Friction and speed control are the heartbeats that keep that system alive. By understanding how materials, load, maintenance, and design influence these factors, you can turn a struggling line into a model of lean efficiency. So the next time you walk past your production floor, take a closer look at that roller track. Is it gliding smoothly? Are parts arriving on time? If not, maybe it's time to give friction and speed the attention they deserve. Your operators (and your bottom line) will thank you.